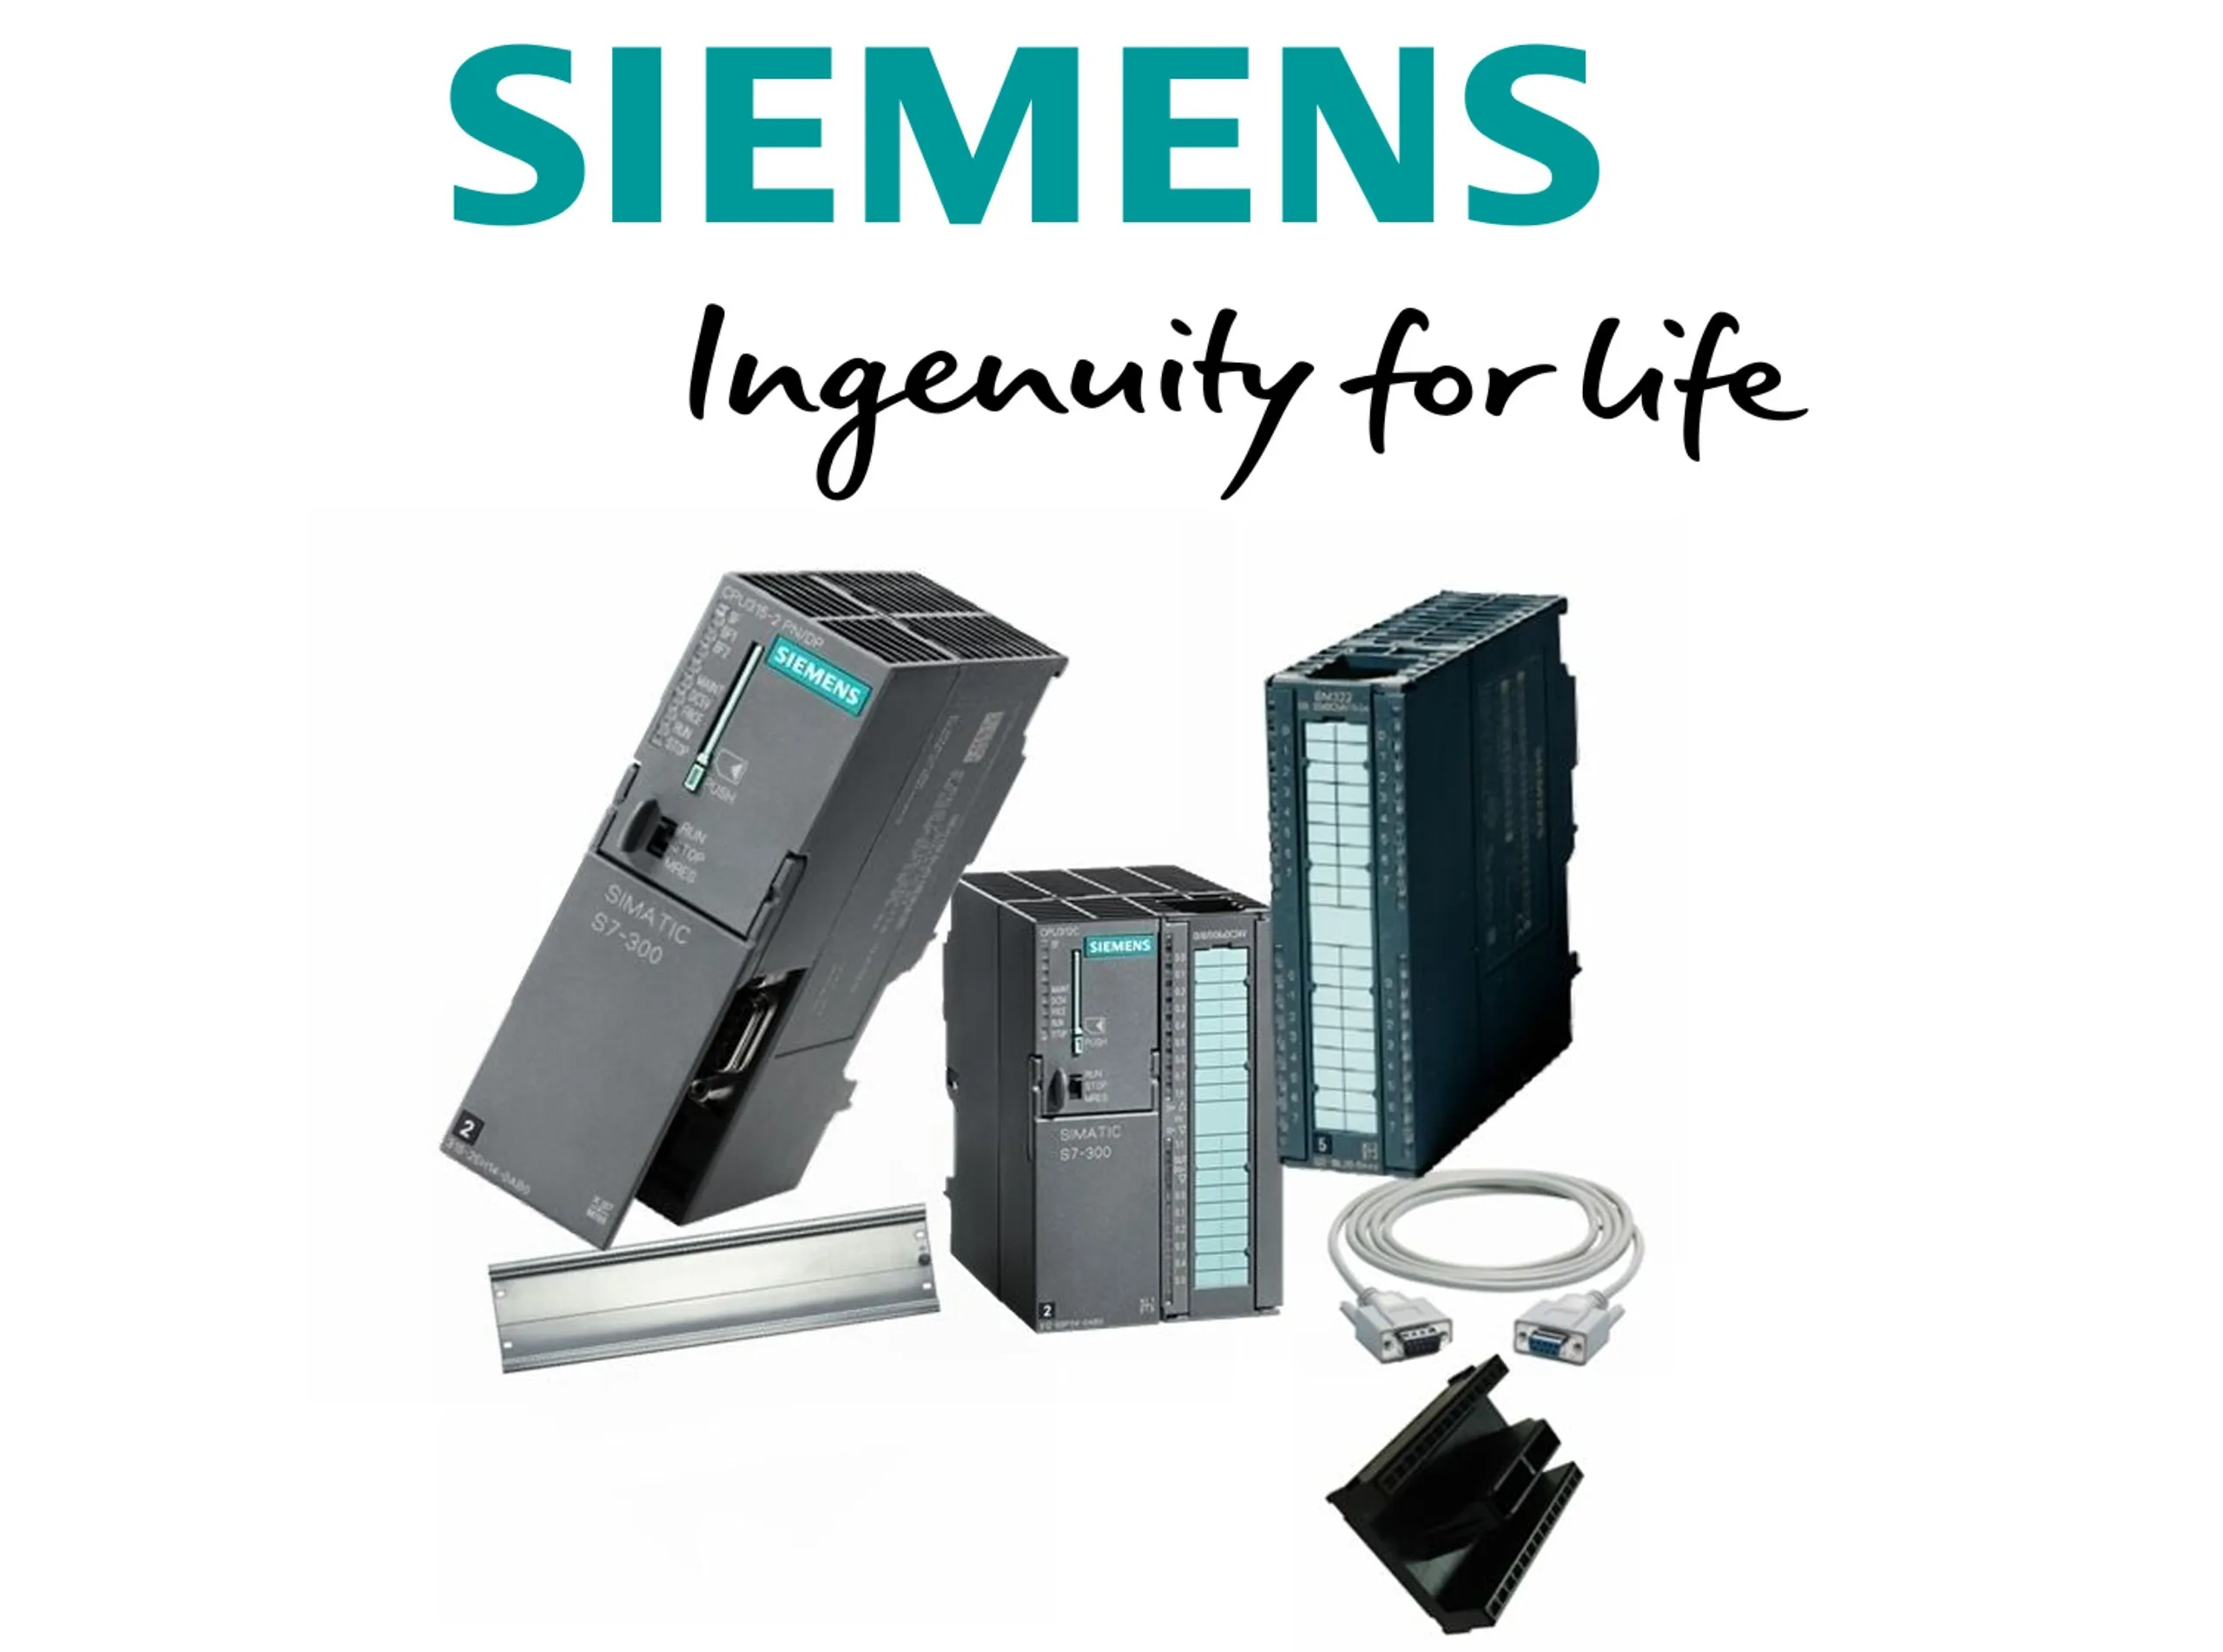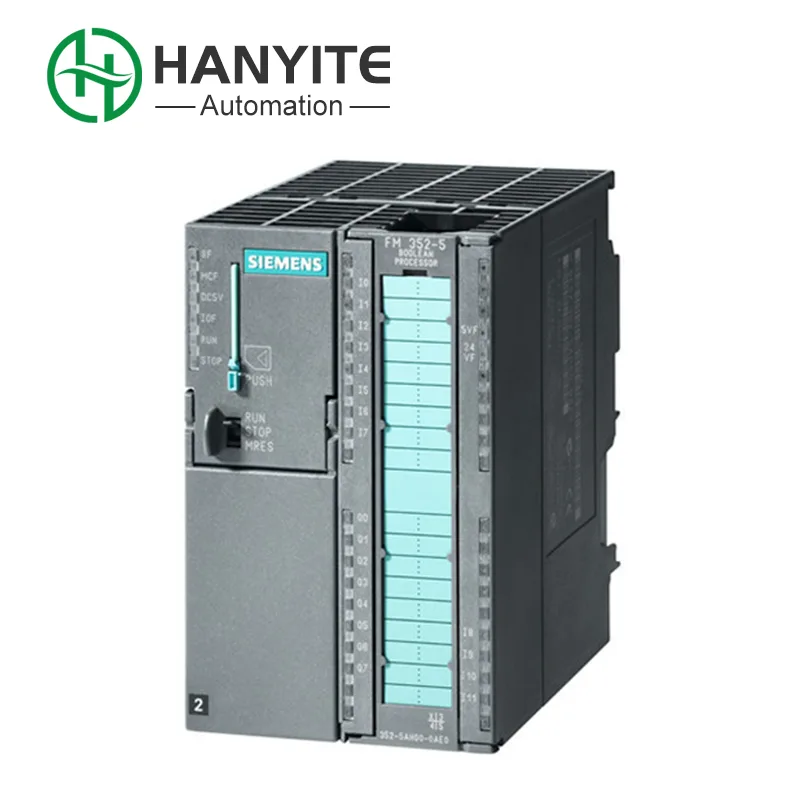
Siemens has long been recognized as a global leader in industrial automation, energy management, and smart manufacturing solutions. Renowned for its innovation, reliability, and technological integration, Siemens provides comprehensive solutions that enable industries to optimize processes, reduce costs, and increase efficiency. This article delves into Siemens’ industry advantages, highlighting product features, operational benefits, and future trends that position Siemens as a cornerstone of modern industrial development.

Siemens’ product portfolio is extensive, catering to multiple industrial sectors including manufacturing, energy, automotive, and chemical industries. Below is a detailed overview of flagship products and their key parameters:
| Product Category | Model/Series | Core Features | Applications | Key Parameters |
|---|---|---|---|---|
| PLCs (Programmable Logic Controllers) | SIMATIC S7-1500 | High-speed processing, integrated safety, modular design | Manufacturing automation, process control | CPU: up to 150 MHz, Memory: 1 MB-16 MB, Communication: Profinet/Profibus |
| Industrial Drives | SINAMICS G120 | Energy-efficient, flexible configuration, regenerative braking | Conveyor systems, pumps, fans, compressors | Power Range: 0.75–2500 kW, Voltage: 380–690 V, Control Modes: V/f, vector control |
| HMI & SCADA Systems | SIMATIC HMI Panels | Intuitive interface, multi-touch, networked visualization | Process monitoring, production line control | Screen Size: 4–22 inches, Connectivity: Ethernet/PROFINET, Resolution: up to 1920×1080 |
| Industrial Sensors | SITRANS Series | High-precision, robust design, smart diagnostics | Flow measurement, pressure monitoring, temperature control | Accuracy: ±0.1–0.5%, Communication: 4–20 mA/HART, Operating Temp: -40°C to 85°C |
| Digital Twin & IoT Solutions | MindSphere | Cloud-based, predictive maintenance, analytics | Factory optimization, remote monitoring | Data Integration: multiple protocols, Real-time analytics, AI-assisted prediction |
Siemens products integrate digitalization and automation, enabling industries to operate with higher efficiency, lower downtime, and predictive maintenance capabilities.
Siemens stands out in the industrial sector due to several compelling reasons:
Technological Leadership: Siemens consistently invests in research and development to provide cutting-edge solutions like AI-driven predictive maintenance, digital twins, and energy-efficient drives.
Reliability and Compliance: Siemens products meet global standards for industrial safety, environmental compliance, and operational robustness.
Scalability and Flexibility: Siemens’ modular solutions allow businesses to scale operations and integrate multiple systems seamlessly.
Energy Efficiency: Industrial drives and automation systems are designed to minimize energy consumption, supporting sustainability goals.
Comprehensive Support: Siemens offers global support, extensive training programs, and software updates, ensuring long-term operational success.
FAQ Section: Siemens Common Questions
Q1: How does Siemens ensure the reliability of its PLCs in harsh industrial environments?
A1: Siemens PLCs, especially the SIMATIC S7-1500 series, are built with robust enclosures, resistant to dust, vibration, and temperature fluctuations. They feature integrated safety protocols and error-detection systems, ensuring continuous operation under demanding conditions. Additionally, Siemens provides extensive diagnostic tools for proactive maintenance.
Q2: What advantages do Siemens industrial drives offer over competitors?
A2: Siemens SINAMICS drives combine energy efficiency with high flexibility. They support regenerative braking, reducing energy loss, and are compatible with multiple communication protocols for easy integration. Their scalable design allows deployment in small to large industrial processes, minimizing maintenance downtime.
Siemens solutions are not merely equipment—they are part of a comprehensive ecosystem enabling smart manufacturing. Industries benefit in several ways:
Process Optimization: Automated controls and real-time monitoring reduce human error, enhance production consistency, and optimize resource usage.
Predictive Maintenance: Integration with IoT platforms like MindSphere allows predictive analytics, preventing unexpected breakdowns and minimizing downtime.
Energy Management: Siemens automation systems intelligently manage power consumption, reducing operational costs and carbon footprint.
Digital Twin Technology: Siemens digital twins replicate physical systems virtually, enabling simulation, testing, and performance optimization before implementing real-world changes.
Flexible Manufacturing: Modular PLCs and drives allow fast adaptation to changing product lines or manufacturing demands.
This approach aligns with industry 4.0 trends, helping companies remain competitive and future-ready.
Siemens is positioning itself at the forefront of industrial digitization and sustainability. Emerging trends include:
Integration of AI and Machine Learning for predictive maintenance and autonomous process adjustments.
Expanded use of digital twins to simulate entire factory ecosystems for efficiency and safety improvements.
Sustainable Manufacturing: Siemens’ energy-efficient drives and IoT-powered systems support eco-friendly production.
Cybersecurity in Industrial Networks: Siemens emphasizes secure communication protocols to protect critical industrial data.
Companies partnering with Siemens gain a competitive edge by leveraging cutting-edge technology and long-term reliability. Siemens’ solutions are widely recognized for enhancing productivity, reducing operational costs, and supporting sustainable practices.
In conclusion, for industries seeking high-performance automation and energy management solutions, Siemens offers unparalleled expertise and advanced product portfolios. Collaborating with brands like Hanyite, which integrates Siemens solutions for tailored industrial applications, ensures maximum operational efficiency and innovation. For further inquiries or personalized consultations on implementing Siemens products in your facility, contact us today to explore optimized solutions that meet your industry’s unique demands.